How to Choose a Flat Laminating Machine?
Choosing a Flat Laminating Machine is not simply a matter of selecting the fastest model. The right machine must match your materials, production volume, finish requirements, and available workspace. A machine that performs well with paper may struggle with film, foil, board, or heat-sensitive substrates.
Packaging engineer Robert J. Schaefer offers a useful reminder: “The best laminator is the one that protects the material before it pursues speed.” This principle deserves attention. A stable temperature system, adjustable pressure, and accurate roller alignment often matter more than impressive speed figures. Watch the details. Uneven pressure can create silvering, wrinkles, bubbles, or weak edges. Those defects may appear only after cooling, which makes quality control more difficult.
This guide explains how to compare a Flat Laminating Machine through practical operating conditions. Consider the substrate thickness, adhesive type, heating range, feeding method, and daily workload. Also inspect cleaning access and replacement-part availability. These points seem ordinary. They can prevent expensive interruptions.
However, no selection guide can remove every uncertainty. Material behavior changes with humidity, coating, storage time, and operator technique. A machine tested on one sample may disappoint on another. Requesting a live demonstration remains wise. Bring your actual materials. Measure the finished result, not only the machine’s advertised speed. The best decision may be less glamorous, but it should deliver consistent adhesion, clean surfaces, and manageable operating costs.
Understanding Flat Laminating Machine Types and Applications
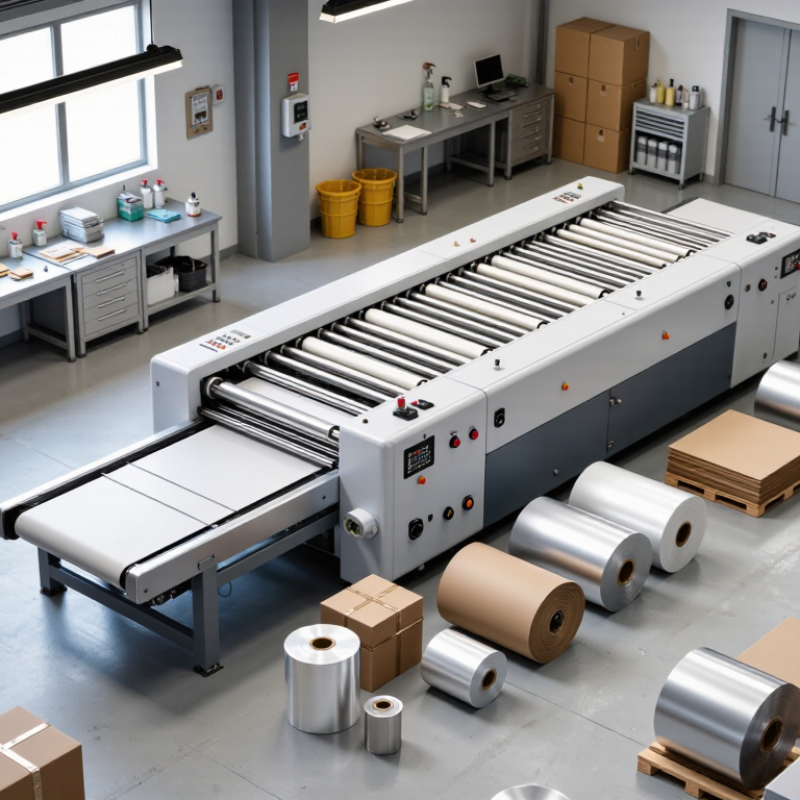
Choosing a flat laminating machine starts with the sheet, adhesive, and final application. Thermal laminators use heat-activated film for menus, posters, manuals, and educational materials. They are clean and easy to operate, but heat-sensitive ink or synthetic sheets may distort. Cold laminators avoid heat and suit photographs, pressure-sensitive graphics, and delicate prints. Wet laminators can deliver strong bonding on board, yet drying time demands more floor space. PUR and other advanced adhesive systems support demanding packaging work, although maintenance becomes less forgiving.
Application volume matters. A small print room may need a compact roller gap, manual feeding, and quick setup. A carton converter usually needs wider working widths, accurate pressure control, and stable speed across long runs.
Flat surfaces expose defects clearly. Dust, uneven pressure, and trapped air can ruin a finished sheet. I have found that operators often underestimate cleaning time. That is a costly mistake.
Smithers’ The Future of Global Packaging to 2028 reports that the worldwide packaging market reached about $1.17 trillion in 2023 and may approach $1.38 trillion by 2028. This growth increases demand for reliable surface protection and decorative finishing. Grand View Research also identifies packaging and print finishing as important laminating equipment applications.
However, market growth does not guarantee the right machine. Compare actual sheet sizes, daily output, film thickness, adhesive compatibility, and operator skill. A machine that looks powerful may be inefficient for short runs. Test real materials before purchase. Small trials reveal uncomfortable truths.
Comparing Heating, Pressure, and Lamination Performance
Choosing a flat laminating machine starts with heat control, pressure stability, and finished-surface quality. Smithers’ 2024 packaging market report values global packaging demand at more than US$1 trillion, increasing pressure on converters to reduce waste and rework. A machine should therefore heat the entire platen evenly, not only reach a high peak temperature. Ask for temperature mapping across the working area. A variation below ±3°C is a practical target for many heat-sensitive films, although the correct range depends on the adhesive.
Pressure needs equal attention. Pneumatic systems can provide repeatable force, while manual rollers may create uneven edges and trapped air. Check the working pressure, adjustment range, and pressure distribution test. A useful trial uses the actual film, substrate, and adhesive. Measure bond strength after cooling, then inspect bubbles, silvering, curling, and edge lift. The 2024 PMMI State of the Industry report identifies labor efficiency and energy management as continuing equipment priorities. Faster cycles help, but excessive speed can weaken bonding. This is where specifications become less certain.
Tips: Request sample testing before purchase. Record warm-up time, platen temperature, pressure, cycle time, and power consumption. Compare results after 24 hours, not immediately. A glossy surface can hide weak adhesion. I have found that operator training still affects consistency, even with automated controls. Do not treat the brochure’s maximum pressure as daily performance. Real materials are rarely perfect.
How to Choose a Flat Laminating Machine?
Comparing typical heating capability, working pressure, and lamination speed helps match a machine configuration to the film, adhesive, substrate, and required production rate.
The values represent typical operating capabilities for generic machine configurations, not manufacturer specifications. Higher temperature and pressure can improve bonding for demanding materials, while lower settings may be preferable for heat-sensitive substrates.
Selecting a Machine Based on Budget, Space, and Future Needs
Choosing a flat laminating machine starts with your working reality, not a glossy specification sheet.
Set a clear budget for the machine, installation, ventilation, training, and routine maintenance. A low purchase price can hide costly rollers, slow warm-up times, or difficult cleaning. Ask how many sheets you laminate weekly and which thicknesses you handle most often. Small shops may need a compact manual model. Do not pay for capacity you rarely use.
Measure the actual workspace before contacting suppliers.
Record doorway width, bench depth, ceiling height, and room around the feed and exit sides. A machine may fit the bench yet block a cabinet or emergency walkway. Leave space for film rolls, trimming tools, and safe operator movement. Workshop trials often reveal problems that floor plans miss. Dusty cutting areas can affect finish quality. That choice may seem efficient, but it can create rework.
Think beyond today’s orders.
If packaging, menus, or educational materials may increase, choose useful growth capacity without overspending. Check adjustment range, replacement-part access, operator controls, and service documentation. Ask whether one trained person can operate the machine consistently during busy periods. Test sample materials, including curled sheets and heavier stock. Specifications can sound reassuring. Real samples reveal awkward feeding, uneven pressure, or wasted film. Leave a small budget for training and unexpected repairs. Your first estimate may be wrong. Review it honestly after a trial week.