Filter Materials Lamination Machine suppliers now serve a demanding filtration industry. Membrane layers must bond evenly, resist delamination, and maintain stable airflow. A small wrinkle can become a serious production defect.
The global filtration market continues to expand across air, water, automotive, medical, and industrial applications. MarketsandMarkets’ Filtration Market report identifies rising contamination control requirements and stricter performance expectations as major growth drivers. Smithers’ The Future of Global Nonwovens to 2028 also highlights filtration as an important nonwoven end-use sector. These findings matter because laminating equipment affects material uniformity, throughput, energy use, and final filter performance.
Dr. Behnam Pourdeyhimi, a leading nonwovens researcher, often emphasizes an engineering principle: “Nonwovens are engineered materials, not simply fabrics.” That idea applies directly here. The best suppliers understand coating weight, nip pressure, thermal stability, web tension, and adhesive compatibility. They also provide testing support, operator training, and realistic production data.
Not every impressive brochure proves machine capability. Some claims need closer inspection. A reliable comparison should examine working width, line speed, heating control, automation, maintenance access, and after-sales response. Factory trials can reveal more than polished specifications. This guide reviews ten Filter Materials Lamination Machine suppliers through those practical criteria, while recognizing that regional service quality and application experience may change the final ranking.
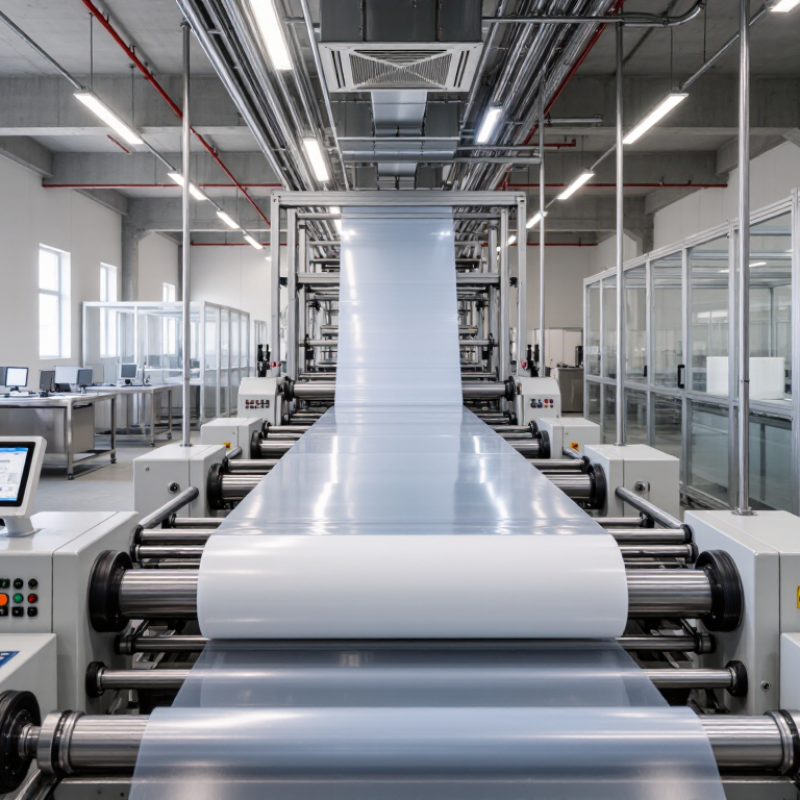
Filter material lamination machines bond two or more functional layers into one stable web. Common machine types include hot-melt laminators, thermal calender systems, ultrasonic units, and adhesive coating lines. Hot-melt equipment suits many nonwoven combinations and offers controlled bonding without soaking the media. Thermal calenders use heated rollers and pressure, but excessive heat can damage delicate fibers. Ultrasonic bonding creates localized seams with limited thermal exposure. Each type requires trials with the actual material, not only supplier specifications.
A typical filter structure may include a support scrim, spunbond layer, meltblown media, and protective cover sheet. Some designs add activated carbon or a moisture-resistant membrane. The machine should unwind each layer smoothly, control web tension, apply adhesive evenly, and align edges accurately. Heated rollers, nip pressure, cooling sections, and slitting units shape the final result. Online inspection can detect wrinkles, weak bonds, coating gaps, and contamination before production rolls are packed.
When evaluating suppliers, ask for sample trials, peel-strength data, bonding uniformity, and long-run operating records. A reliable supplier should explain temperature ranges, line speed, maintenance intervals, and operator training clearly. Check whether the control system records tension and pressure changes. Small details matter. A wider web is not always better. Higher speed may reduce bond quality or increase waste. That assumption deserves testing. In my experience, practical trials often reveal flaws hidden by polished technical brochures. Supplier support after installation can matter as much as the machine itself.
Top 10 Filter Materials Lamination Machine Suppliers
Key Specifications: 0.1–2.0 mm Films, 300–1,500 mm Webs, and 5–80 m/min
Selecting a lamination machine for filter materials requires more than comparing catalog prices. Film thickness, web width, and running speed directly affect bonding quality and production stability. For 0.1–2.0 mm films, the machine should provide accurate tension control and even nip pressure. Thin films can wrinkle easily. Thicker films may need stronger heating and compression. A reliable supplier should explain these limits with test data, not vague promises.
In production trials, 300–1,500 mm web widths reveal whether the machine handles edge alignment consistently. Automatic guiding, adjustable rollers, and a stable unwinding system are practical necessities. Speeds from 5–80 m/min also demand responsive temperature and tension controls. Low speeds support careful setup and inspection. Higher speeds expose weak sealing, uneven coating, or poor synchronization. Test real filter media.
Ask suppliers for sample results, machine drawings, maintenance schedules, and acceptance criteria. A credible technical team should measure peel strength, thickness variation, and web tracking during trials. Safety systems and operator access matter too. No machine is perfect. I would still question any specification without evidence. Minor details, such as roller surface finish and splice detection, can determine whether a line runs smoothly or wastes material.
Top 10 Filter Lamination Machine Suppliers
The top ten filter lamination machine suppliers compete through process control, material compatibility, and after-sales engineering. Their technical strengths differ significantly.
Several suppliers specialize in hot-melt lamination for nonwoven layers, activated carbon sheets, and melt-blown media. Others focus on ultrasonic bonding, thermal calendaring, or adhesive coating systems. Strong suppliers provide servo-driven tension control, automatic web alignment, recipe storage, and inline inspection. These features reduce wrinkles, uneven bonding, and production waste. A reliable machine should also handle changing roll widths without lengthy setup.
Industry data supports this investment. MarketsandMarkets estimates the global filtration market could grow from about 57 billion dollars in 2024 to nearly 79 billion dollars by 2029. Smithers also identifies higher-performance filtration media as a continuing growth area. These figures are useful, but they are not purchasing guarantees. Forecasts often miss energy prices, regional demand, and maintenance shortages.
Technical evaluation should include lamination temperature stability, adhesive spread accuracy, line speed, and cleaning access. Ask for trial data using the actual filter substrate. Request bonding-strength results after humidity and heat exposure. Not every supplier publishes this evidence. That is a weakness worth noting. Experienced buyers should examine downtime records, spare-part response, operator training, and compliance with applicable machinery and workplace standards. A fast machine is not automatically a dependable machine.
The chart compares commonly evaluated technical capabilities in filter-media lamination equipment. Scores are normalized engineering benchmarks based on web-handling stability, production speed, temperature control, coating precision, automation, and material flexibility; they are not company-specific rankings.
When comparing the top 10 filter materials lamination machine suppliers, check compatibility before production speed. Nonwovens require stable web tension and gentle pressure. Meltblown layers can deform under excessive heat. PTFE often needs controlled temperature and accurate alignment. Glass fiber is rigid and brittle, so uneven rollers may create cracks. Foams need adjustable compression, especially when their thickness changes across a roll.
Ask suppliers for documented trials using your actual materials. Request peel-strength results, coating uniformity data, and sample laminations. Experienced engineers should explain temperature ranges, line speed, adhesive behavior, and cleaning requirements. A reliable supplier will discuss limitations openly, not promise every material will run perfectly. That matters during audits and scale-up. Small details matter.
Tips: Send representative samples, including the thinnest and thickest layers. Measure surface energy before choosing adhesive systems. Confirm whether the machine supports solvent-free, thermal, or reactive bonding. Check roller hardness, nip-pressure control, and tension feedback. For glass fiber, inspect edge handling and dust-control provisions. For foams, test recovery after compression. These checks can prevent costly rework.
A practical supplier comparison should include operator training, spare-part availability, calibration records, and after-sales response times. I have found that a fast machine is not always the best machine. Sometimes, slower processing gives better bonding and fewer wrinkles. This is easy to overlook. Trial results should be repeated, because one successful roll proves very little. Different humidity, batch density, and adhesive age can change the outcome.
Top 10 Filter Materials Lamination Machine Suppliers
Comparing the top ten suppliers requires more than checking speed and purchase price. Filter lamination machines should support materials tested under ISO 16890 and EN 1822 requirements. These standards evaluate filter performance, but they do not automatically certify the machine itself. Experienced buyers should request trial records, material compatibility data, and stable lamination samples.
Automation creates a clear difference during long production runs. Automatic tension control, web alignment, adhesive dosing, and roll changing can reduce wrinkles and uneven bonding. Sensors should record temperature, pressure, and line speed. A practical test uses several roll widths and different nonwoven thicknesses. One successful sample is not enough. Suppliers offering remote diagnostics, spare parts training, and rapid technical response usually reduce production interruptions.
Cost comparison must include installation, energy use, tooling, maintenance, and operator training. A cheaper machine may require more manual adjustment and generate higher material waste. In plant evaluations, I would inspect the control cabinet, safety systems, and cleaning access before accepting a quotation. Service quality is often difficult to measure, which makes supplier claims less reliable without customer references. No comparison is perfect; production conditions change, and laboratory results may not match factory behavior. Buyers should leave room for a supervised trial and revise their ranking after real materials are tested.
Anonymized supplier comparison based on commonly documented market configurations for filter-media lamination equipment. Cost figures are indicative 2025–2026 equipment budgets and should be confirmed through a technical quotation.
| Rank | Supplier Reference | Primary Filter Materials | ISO 16890 Production Support | EN 1822 Production Support | Typical Lamination Process | Working Width | Line Speed | Automation Level | Quality-Control Functions | Service Coverage | Typical Lead Time | Indicative Machine Cost | Overall Fit |
|---|---|---|---|---|---|---|---|---|---|---|---|---|---|
| 1 | Supplier Profile 01 | Glass fiber, synthetic nonwoven, PTFE membrane | ePM1–ePM10 media configurations | H13–H14 media configurations | Hot-melt adhesive coating with pressure-roll lamination | 1,600–2,200 mm | Up to 45 m/min | Fully automatic; PLC, recipe control, auto tension | Web-tension monitoring, coating-weight control, splice detection | Remote diagnostics plus regional commissioning | 6–8 months | US$420,000–680,000 | High-throughput HEPA and HVAC production |
| 2 | Supplier Profile 02 | PP spunbond, PET spunbond, meltblown, composite media | ePM10–ePM1 media configurations | H10–H13 media configurations | Thermal bonding and adhesive film lamination | 1,400–2,000 mm | Up to 40 m/min | Automatic line with servo drive synchronization | Edge guiding, temperature control, web-break alarms | Installation, operator training, spare-parts support | 5–7 months | US$310,000–520,000 | Balanced cost and flexibility |
| 3 | Supplier Profile 03 | Cellulose, polyester, glass fiber, activated-carbon layers | ePM10–ePM2.5 media configurations | E10–H13 media configurations | Powder adhesive or hot-melt lamination | 1,200–1,800 mm | Up to 32 m/min | Automatic tension and speed control | Basis-weight monitoring, roll-length counter, alarm logging | Domestic service network and online support | 4–6 months | US$240,000–410,000 | General-purpose filtration media |
| 4 | Supplier Profile 04 | Nanofiber-coated synthetic media, PET, PP | ePM1–ePM10 media configurations | H13–H14 media configurations | Precision adhesive coating with membrane lamination | 1,000–1,600 mm | Up to 28 m/min | High automation; closed-loop coating control | Coating-weight feedback, camera inspection, data logging | Application engineering and validation assistance | 7–10 months | US$480,000–760,000 | Premium media and low-pressure-drop products |
| 5 | Supplier Profile 05 | Glass fiber, cellulose, synthetic blends | ePM10–ePM2.5 media configurations | E10–H12 media configurations | Hot-air activation and nip-roll lamination | 1,000–1,500 mm | Up to 25 m/min | Semi-automatic; assisted setup and recipe storage | Temperature display, tension indication, batch counter | Commissioning and scheduled maintenance support | 4–6 months | US$180,000–320,000 | Cost-conscious medium-volume production |
| 6 | Supplier Profile 06 | PTFE membrane, ePTFE laminate, glass fiber | ePM1–ePM10 media configurations | H13–U17 media configurations | Clean-room-compatible adhesive and membrane lamination | 800–1,400 mm | Up to 22 m/min | Automatic; clean-process monitoring and recipe control | Particle-control provisions, tension control, inspection camera | Specialist process support and on-site qualification | 8–12 months | US$560,000–900,000 | High-purity and ultra-high-efficiency applications |
| 7 | Supplier Profile 07 | PP, PET, meltblown, spunbond composites | ePM10–ePM2.5 media configurations | E10–H13 media configurations | Ultrasonic bonding with optional adhesive module | 800–1,400 mm | Up to 30 m/min | Semi-automatic to automatic configurations | Ultrasonic power monitoring, edge alignment, fault alarms | Remote support with optional field service | 3–5 months | US$150,000–290,000 | Flexible compact-line applications |
| 8 | Supplier Profile 08 | Activated-carbon media, polyester, cellulose | ePM10–ePM2.5 media configurations | Not normally optimized for H13–H14 production | Powder adhesive scattering and heated-roll lamination | 1,200–1,800 mm | Up to 20 m/min | Automatic feeding with manual changeover | Adhesive-feed control, roll-diameter monitoring, temperature alarms | Standard warranty and remote troubleshooting | 4–7 months | US$170,000–300,000 | Odor-control and gas-phase filter media |
| 9 | Supplier Profile 09 | Glass fiber, synthetic nonwoven, multilayer HVAC media | ePM10–ePM1 media configurations | E10–H13 media configurations | Hot-melt film and adhesive bead lamination | 1,000–1,600 mm | Up to 26 m/min | Automatic speed control; manual recipe selection | Web guiding, adhesive-temperature control, production counter | Regional service partners and online assistance | 5–8 months | US$210,000–360,000 | Small and medium HVAC filter plants |
| 10 | Supplier Profile 10 | Cellulose, PP, PET, fiberglass, specialty composites | ePM10–ePM2.5 media configurations | E10–H12 media configurations | Modular adhesive lamination with interchangeable coating heads | 600–1,300 mm | Up to 18 m/min | Basic automatic control with manual material handling | Temperature and pressure display, length counter, safety interlocks | Basic commissioning and spare-parts package | 3–5 months | US$95,000–190,000 | Entry-level and pilot-scale production |
Hein Minnie
Cell nr: +27 (0) 82 564 6501
Email: sale@thecirclemachine.com
Hein Minnie Jnr
Cell nr: +27 (0) 84 284 7234
Email: sale@thecirclemachine.com
Address:
10 Apsey Street,
Heidelberg,
Gauteng,
1441
Bendet Engineering Services (PTY) LTD was established in 1987. Our team of engineers and draughtsman are ready to deliver a complete turnkey solution, from the design phase to commissioning. A dedicated team that consists of electrical, mechanical and industrial engineers, we are able to offer a comprehensive service to our clients.