10 Powder Coating Tips for Buyers

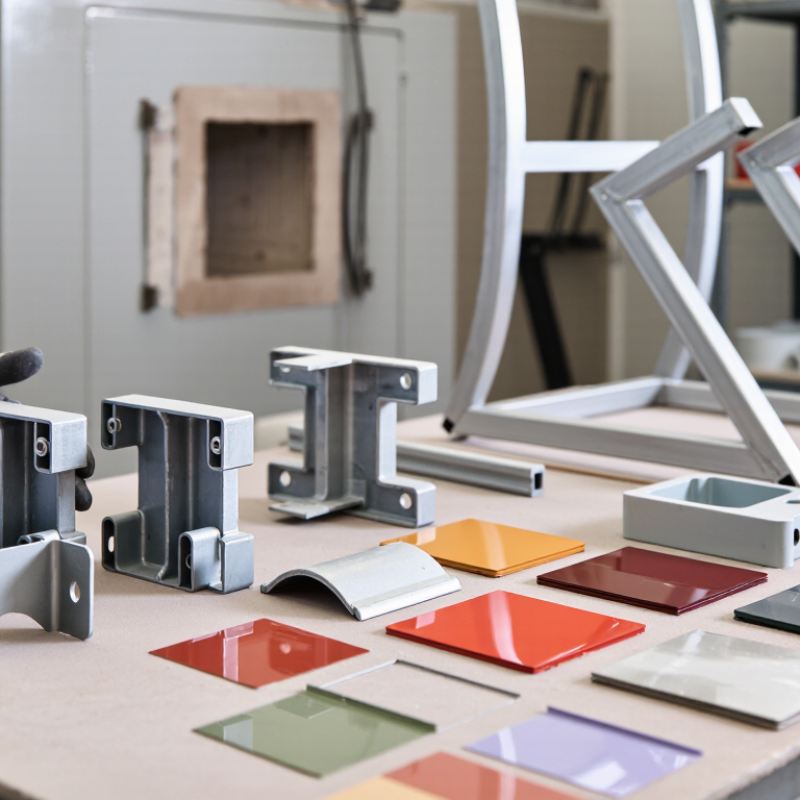
Choosing powder coating for a product involves more than picking a color from a chart. Buyers also need to consider the part’s material, shape, intended use, and exposure to weather or handling. A small steel bracket for indoor shelving has different needs from an aluminum patio frame. Details matter. Ask suppliers how they prepare surfaces, control film thickness, and check finished parts. A smooth sample can look convincing, but it may not reveal how the coating performs around edges, corners, or threaded holes.

These ten buyer tips will help you compare quotes and ask more useful questions. Request a sample on the same substrate when possible, and inspect its color, texture, and coverage under ordinary lighting. Clarify what the quoted price includes, such as pretreatment, masking, packaging, and delivery. Ask about typical lead times and how rejected parts are handled. Technical data sheets can provide useful information, but match their test conditions to your actual application. A coating’s advertised durability is not a guarantee for every environment. That assumption can be wrong. It is also easy to focus on the lowest price and overlook inconsistent preparation or limited inspection. Not every buyer needs the most demanding specification. Still, a little extra checking before an order can prevent visible defects, delays, and costly rework. Use the tips as a practical starting point, then confirm requirements with a qualified coating supplier.
10 Powder Coating Tips for Buyers

Set Substrate and Exposure Requirements Before Comparing Powder Coats

10 Powder Coating Tips for Buyers

Set Substrate and Exposure Requirements Before Comparing Powder Coats

Start with the part, not the finish. Identify whether it is steel, aluminum, or another substrate, and note its thickness and shape. A sharp corner, recessed channel, or welded seam can affect coating coverage. Record the existing surface condition, too. Oil, rust, and leftover scale may interfere with adhesion.

Then describe where the part will work. Will it sit indoors, face direct sunlight, or encounter rain and salt spray? Note contact with cleaners, oils, heat, or frequent handling. Be specific: a railing near a coastal walkway has different exposure than a cabinet in a dry warehouse. “Outdoor use” alone tells a supplier very little. Small details count.

Share these conditions with coating suppliers before comparing color, price, or gloss. Ask what pretreatment and film thickness they recommend for the substrate and service environment. Request test panels made with a similar metal and preparation process, then inspect them for color, coverage, and adhesion. A sample can look convincing on a flat coupon, yet behave differently around edges. That difference is easy to miss. Keep the requirements in writing, but revisit them if the part’s use changes.
Choose Resin Chemistry: Polyester for UV Exposure, Epoxy for Interiors

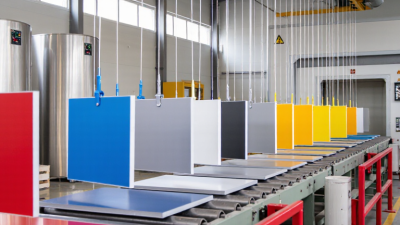
For outdoor parts, polyester powder is usually the safer starting point. It generally retains color and gloss better under sunlight than epoxy. Think of a railing facing south, where afternoon sun can expose weak coatings quickly. Polyester can still fade over time, especially in harsh conditions. Ask for weathering data that matches the exposure, rather than relying on a generic “outdoor” claim.

Epoxy is often a strong fit for interior components. It can provide good adhesion and resistance to many chemicals, which helps on shelves, cabinets, or equipment housings. But direct sunlight is a weakness: epoxy may chalk and lose its appearance outdoors. That rule is useful, but not complete. Indoor parts near windows, wash-down areas, or heat sources may need a closer review of the service conditions.

Check more than resin type. Confirm the part’s operating temperature, cleaning agents, expected abrasion, and required finish. A glossy sample can look convincing under showroom lights; inspect it under the lighting and handling conditions it will actually face. Also confirm that the curing schedule suits the part’s thickness and metal substrate. Small test panels help. They do not guarantee years of performance, but they can reveal poor adhesion or an unsuitable appearance before a full production run.

Specify Film Build: 50–100 μm Is Common; Follow the Product Data Sheet

Treat 50–100 μm as a common starting range, not a universal requirement. The right film build depends on the powder, part geometry, and exposure conditions. Check the product data sheet for its recommended thickness and cure schedule before placing an order. Do not assume that a thicker coating automatically provides better protection. Excess material can affect appearance, fit, or curing.

Measure the cured coating with a suitable dry-film thickness gauge. Confirm the gauge is appropriate for the substrate, and check it against its calibration standards. Take readings at several locations, including broad flat areas and spots near edges or recesses. These areas may not receive powder evenly. Keep a simple record of the readings and inspection points. It helps reveal patterns.

Small variations are normal. A single reading rarely tells the whole story. If results fall outside the data sheet’s guidance, discuss the application setup with the coater before changing the target. Sometimes the part shape is the issue, not the powder amount. And honestly, a neat average can hide thin spots. Check the range, not just the average.

Verify Cure at Part Temperature: Many Powders Cure at 160–200°C

10 Powder Coating Tips for Buyers

Verify Cure at Part Temperature: Many Powders Cure at 160–200°C

A powder’s cure schedule refers to the part’s temperature, not the oven’s air setting. That distinction matters. A panel may sit in a 180°C oven while its metal remains cooler, especially when the load is thick or tightly packed. Ask the supplier for the recommended temperature and dwell time, then confirm both against the product’s technical data sheet.

Use a contact thermocouple on a representative part, ideally at a thick section or a cool area far from the heat source. A data logger can show how long the metal takes to reach the target temperature. Start the cure-time count only after the part reaches the specified temperature. Small details count. Door openings, crowded racks, and changing part thickness can alter the heating curve.

Do not rely on a single test panel. Check parts from different rack positions, then assess finish, adhesion, and impact resistance using suitable quality checks. Undercuring can leave a coating soft or poorly bonded; excessive heat may discolor or damage it. The stated 160–200°C range is only a guide, not a universal recipe. Powder chemistry and part design vary. In practice, the oven display can look reassuring while the part tells a different story. That is easy to overlook, and worth checking again.

Check Film Thickness and Adhesion: ASTM D7091 and ASTM D3359 (0B–5B)

10 Powder Coating Tips for Buyers

A glossy panel can still hide a thin or poorly bonded film. Ask suppliers to measure dry-film thickness using ASTM D7091, which covers magnetic and eddy-current gauge methods on metal substrates. Verify the gauge against certified shims and the actual uncoated substrate; a reading on a different metal can mislead. Many powder systems specify roughly 50–75 μm, but this is not a universal target. Check the coating specification and record readings at several points, including edges and recesses. One reading is not enough.

For adhesion, ASTM D3359 Method B uses a cross-cut and pressure-sensitive tape. Its rating runs from 0B to 5B: 5B means no coating was removed, while 0B means more than 65% was removed. The intermediate ratings correspond to increasing removed area. Test only after the specified cure and conditioning; otherwise, the result may reflect process timing, not service performance. Keep the cut spacing appropriate to film thickness, and photograph the grid before and after tape removal. Small details matter. This test is comparative, not a direct measurement of bond strength, and a clean result on a flat coupon may not predict adhesion around a sharp edge. Ask for the test method, readings, and acceptance limit in writing. My own caution: buyers sometimes request a perfect score without defining the test conditions. That leaves room for avoidable disagreement.

10 Powder Coating Tips for Buyers - Check Film Thickness and Adhesion: ASTM D7091 and ASTM D3359 (0B–5B)
No. Buyer Tip What to Specify or Check Test Method or Tool Practical Guidance
1 Set a target dry film thickness (DFT). State the required minimum, target, and maximum DFT in micrometres (µm), and identify the measurement locations. ASTM D7091; magnetic or eddy-current thickness gauge, selected for the substrate. A commonly encountered powder-coating range is approximately 60–100 µm (2.4–3.9 mil), but the correct limit depends on the coating system, part design, and performance specification.
2 Do not treat a typical range as an acceptance limit. Use the product data sheet, purchase specification, or agreed drawing requirement to define acceptance. ASTM D7091 provides measurement practices; it does not prescribe one universal acceptable coating thickness. Confirm whether the requirement applies to each reading, an average, or a defined sample plan. Agree on the decision rule before production.
3 Match the gauge to the base material. Identify whether the coating is on a ferrous or non-ferrous metal substrate. Magnetic induction gauges are used on ferrous substrates; eddy-current gauges are used on non-ferrous conductive substrates. Check gauge suitability, probe access, and substrate condition. Roughness, curvature, and small or narrow parts can affect readings.
4 Verify the gauge before taking measurements. Ask for documented verification and suitable reference standards or certified shims. Follow ASTM D7091 and the gauge manufacturer’s instructions for verification and adjustment. Verify on an uncoated substrate representative of the part when possible. Record the gauge identification and verification results with the inspection data.
5 Measure representative areas, not just easy-to-reach surfaces. Agree on a sampling plan covering flat areas and relevant edges, recesses, or other critical locations. Take multiple readings at agreed locations and report individual results as well as any calculated average. Geometry and electrostatic application can create thickness variation. Avoid assuming one reading represents the entire part.
6 Check adhesion using an agreed procedure. Specify the test method, test area, conditioning, tape procedure, and acceptance rating in advance. ASTM D3359; Method A uses an X-cut, and Method B uses a cross-cut lattice. Method selection depends on the coating and application. Follow the current standard and the project specification rather than choosing a method only for convenience.
7 Understand the ASTM D3359 rating scale. Record the rating from 0B through 5B and the test method used. Method B rating guide: 5B, no coating removed; 4B, less than 5% affected; 3B, 5–15%; 2B, 15–35%; 1B, 35–65%; 0B, more than 65% affected. These ratings describe coating removal in the test area. State the required minimum rating separately; the standard does not make one rating a universal pass level.
8 Use a suitable test area and prepare it consistently. Confirm that the surface is clean and that the location is appropriate for the selected cut pattern and tape. Perform the test according to the applicable ASTM D3359 method and the agreed inspection procedure. Cut quality, tape application, removal technique, and surface condition can influence results. Do not compare results obtained using different procedures as if they were identical.
9 Evaluate cure as well as appearance. Agree on the coating manufacturer’s specified cure schedule, including part-metal temperature and time where applicable. Use a documented oven or process record; select any additional cure test through the coating specification. Oven air temperature alone does not confirm that the part reached its required temperature. Adhesion results can be affected by inadequate cure or poor surface preparation.
10 Request traceable inspection records. Include part or lot identification, measurement locations, DFT readings, gauge details, adhesion method and rating, and inspection date. Review results against the agreed purchase specification and sampling plan. Ask that any nonconforming results, retests, and corrective actions be documented. Keep the acceptance criteria consistent across orders.
Note: Thickness ranges and examples in this table are general buyer guidance, not universal acceptance criteria. Confirm applicable standard editions, coating requirements, substrate conditions, and acceptance limits in the contract or technical specification.
Open chat
Scan the code
Bendet Sales Assistant
Hi There👋,
Thank you for visiting our website, How can I help you?